If you have a need to contact us, email us at [email protected] or use the form below.
We look forward to serving you!
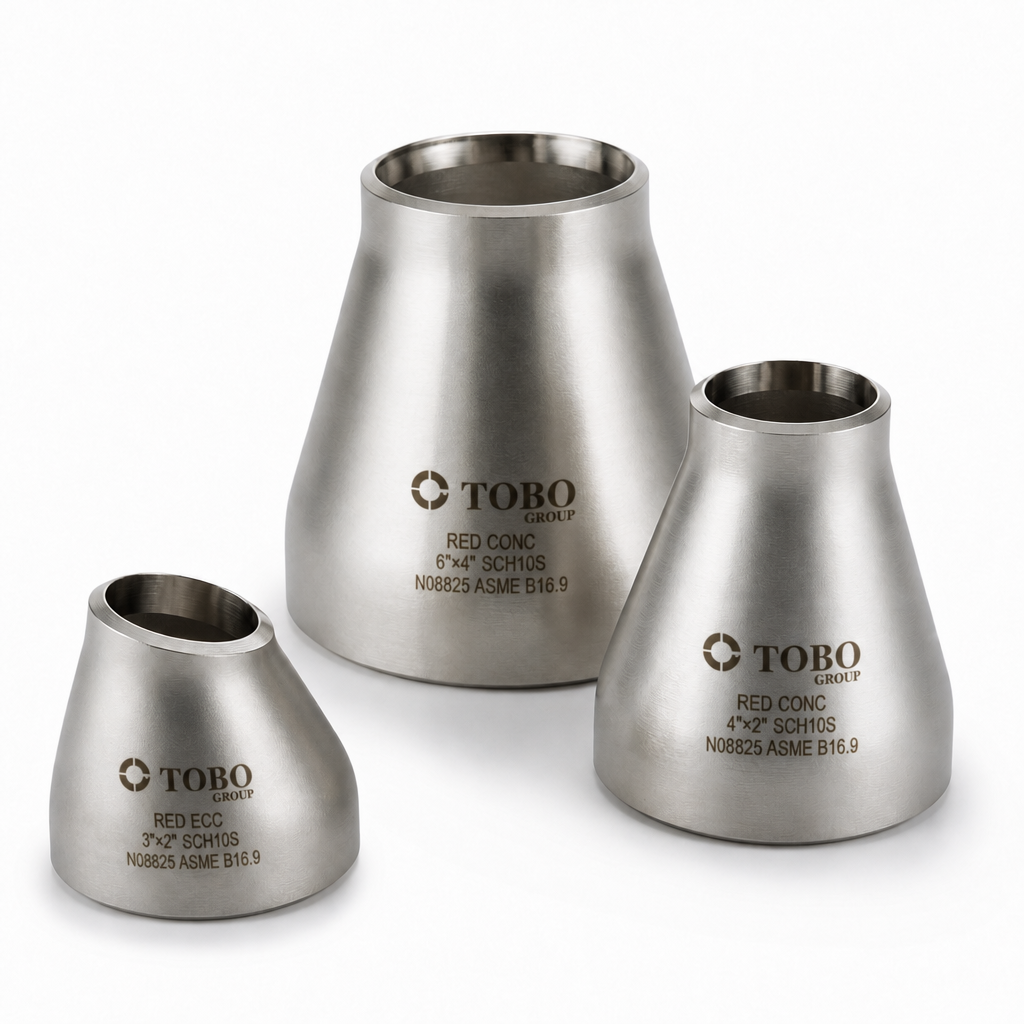
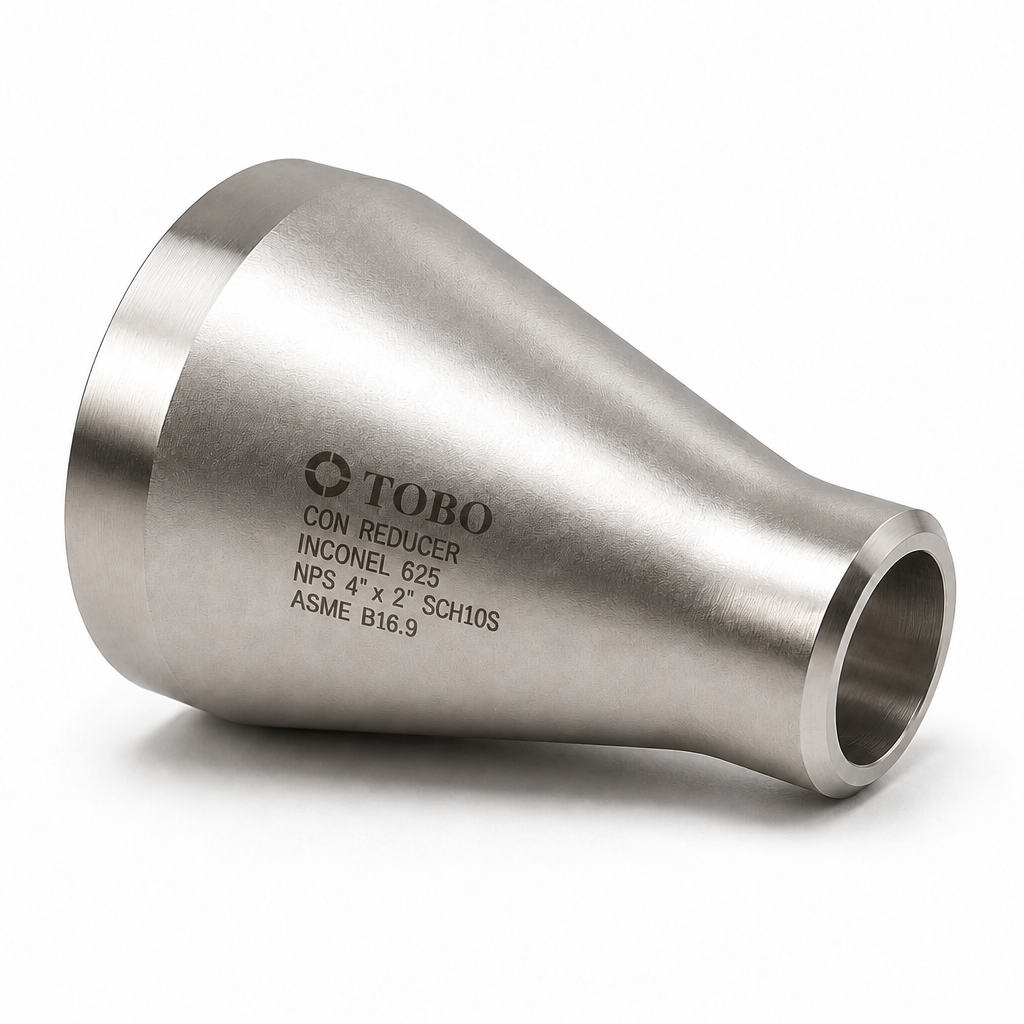
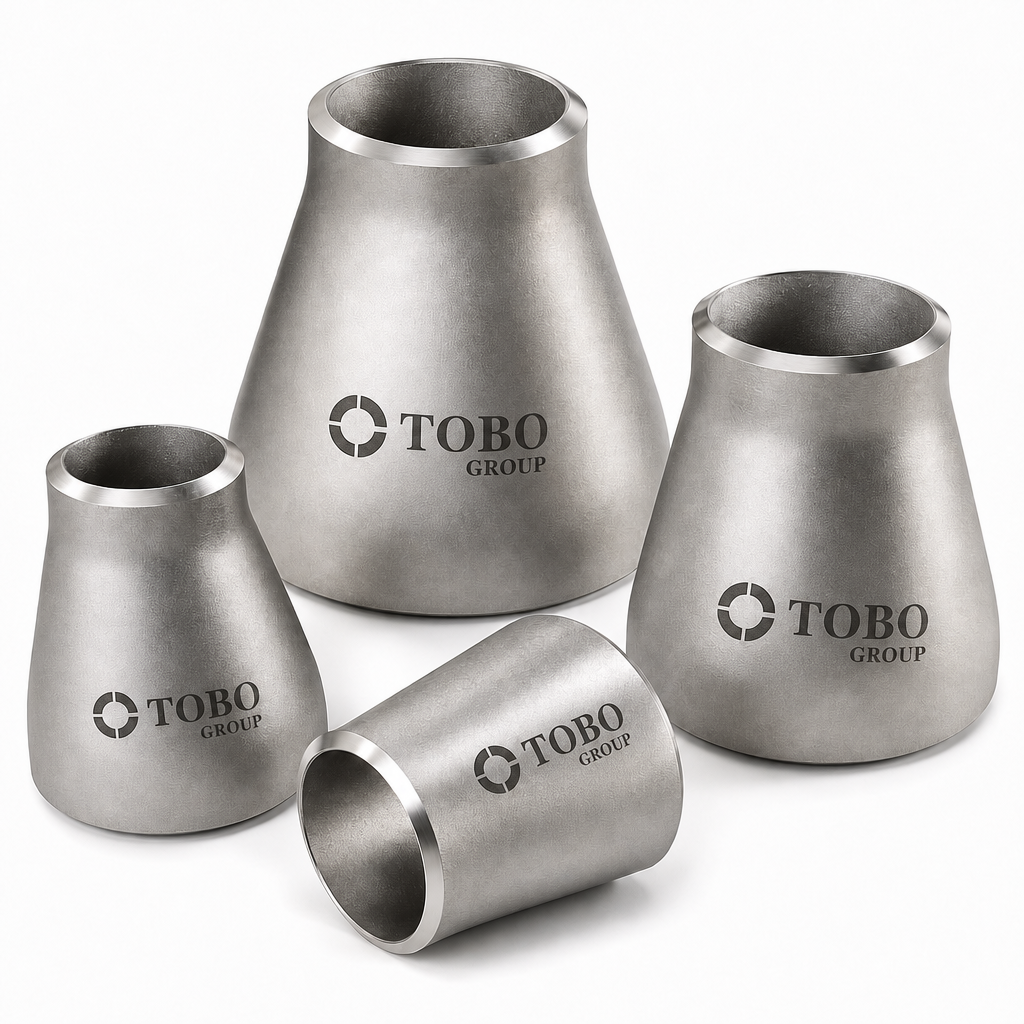
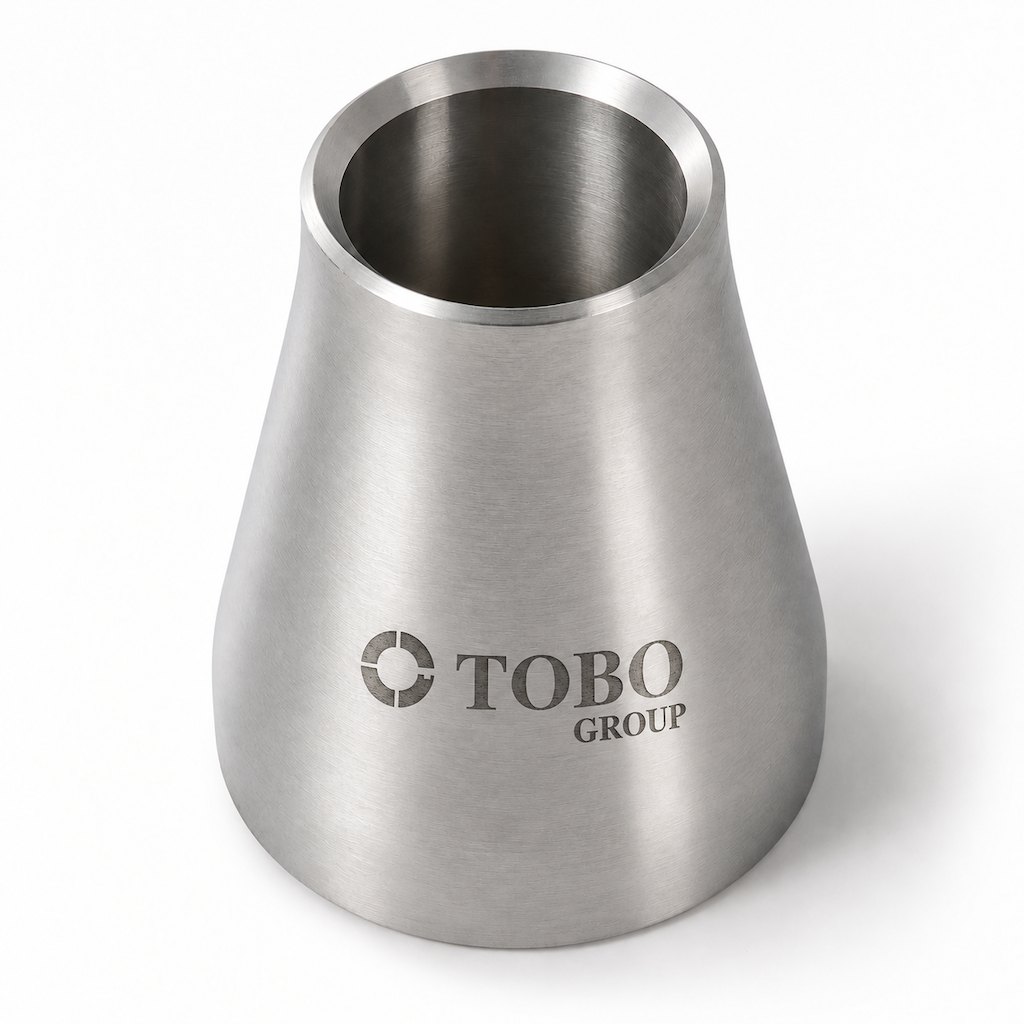
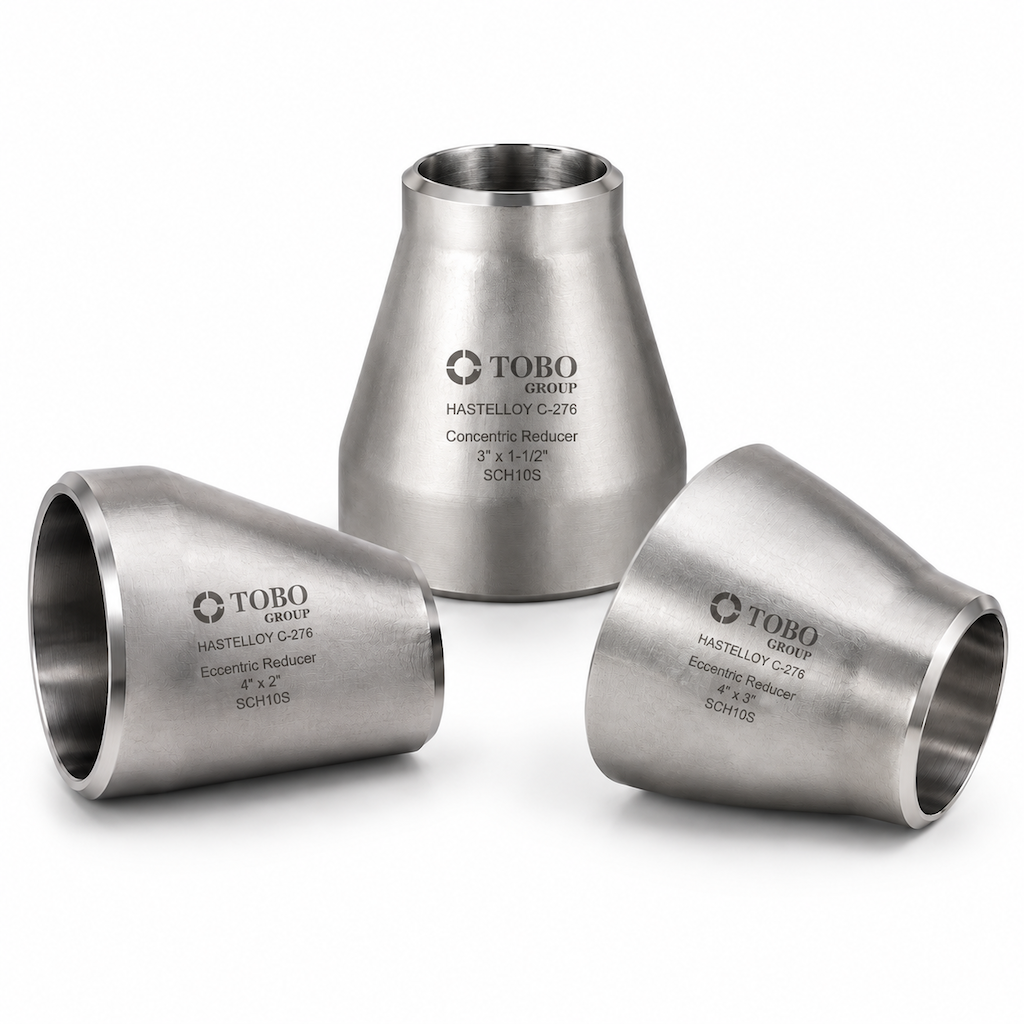
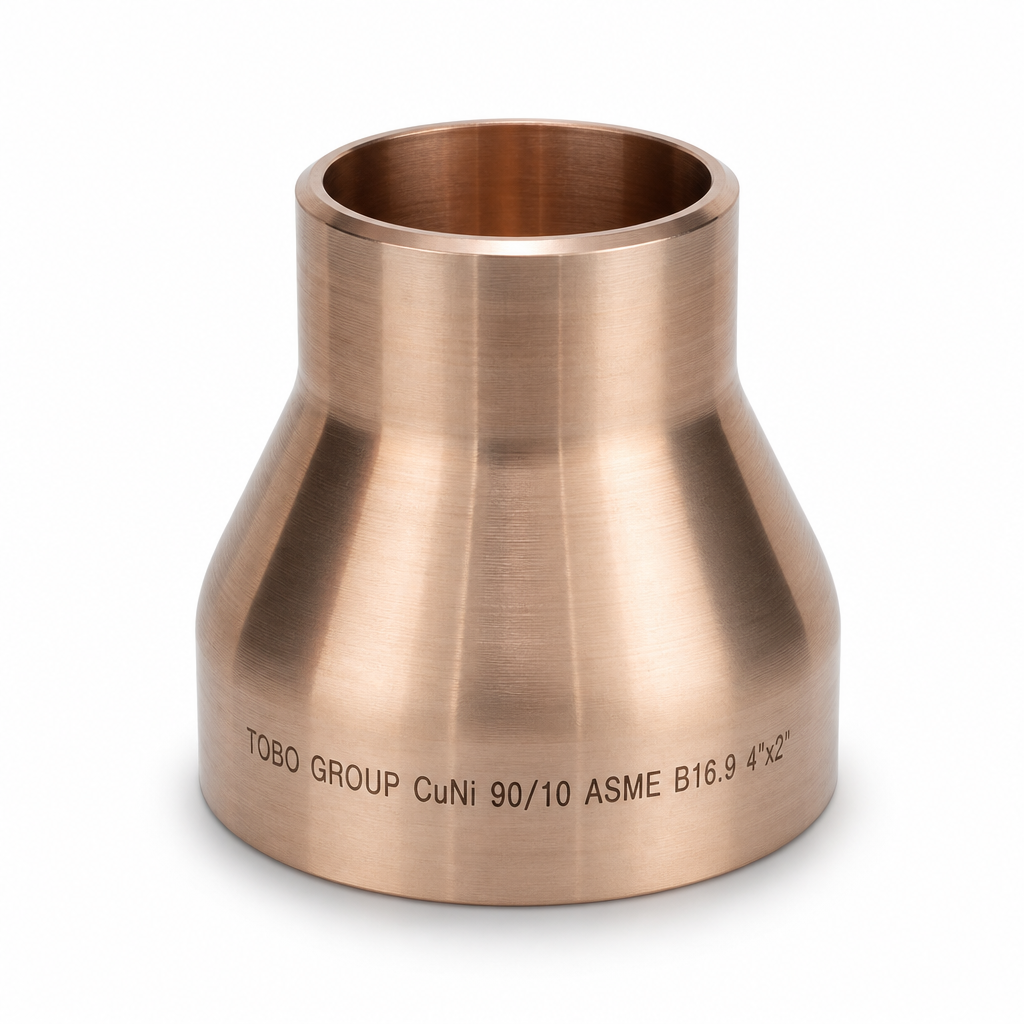
Industrial Nickel Alloy Corrosion-Resistant Reducer Fittings
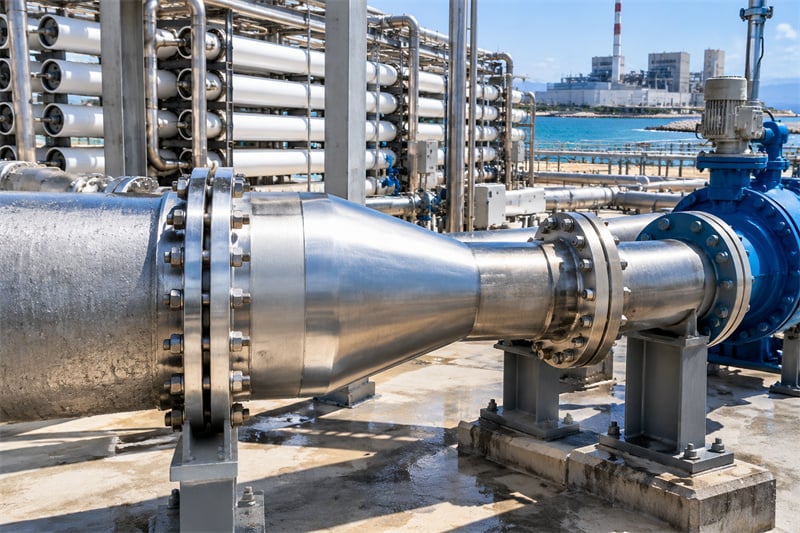
Industrial-grade corrosion-resistant nickel alloy reducers (reducing elbows) are critical pipeline transition components specifically designed for extremely harsh operating conditions and are available in both concentric and eccentric configurations. The products are manufactured from Hastelloy C-276/C-22, Inconel 625/600, Incoloy 825/800H, Monel 400, and pure nickel (Nickel 200/201). Manufactured using precision seamless extrusion and butt-welding processes, these products strictly comply with ASME B16.9, ASTM B366, and NACE MR0175 standards. This series of pipe fittings exhibits exceptional resistance to general corrosion, pitting corrosion, crevice corrosion, and stress corrosion cracking (SCC) in environments containing strong acids and alkalis, moist chlorine gas, hydrogen sulfide (H₂S), and high chloride ion concentrations. They also demonstrate excellent mechanical stability at both high and low temperatures, as well as superior hydrodynamic performance against erosion, and are widely used in offshore oil and gas engineering, petrochemicals and fine chemicals, flue gas desulfurization (FGD), nuclear power, and high-purity pharmaceuticals—core industrial piping networks with stringent requirements for corrosion resistance, lifespan, and pressure safety.
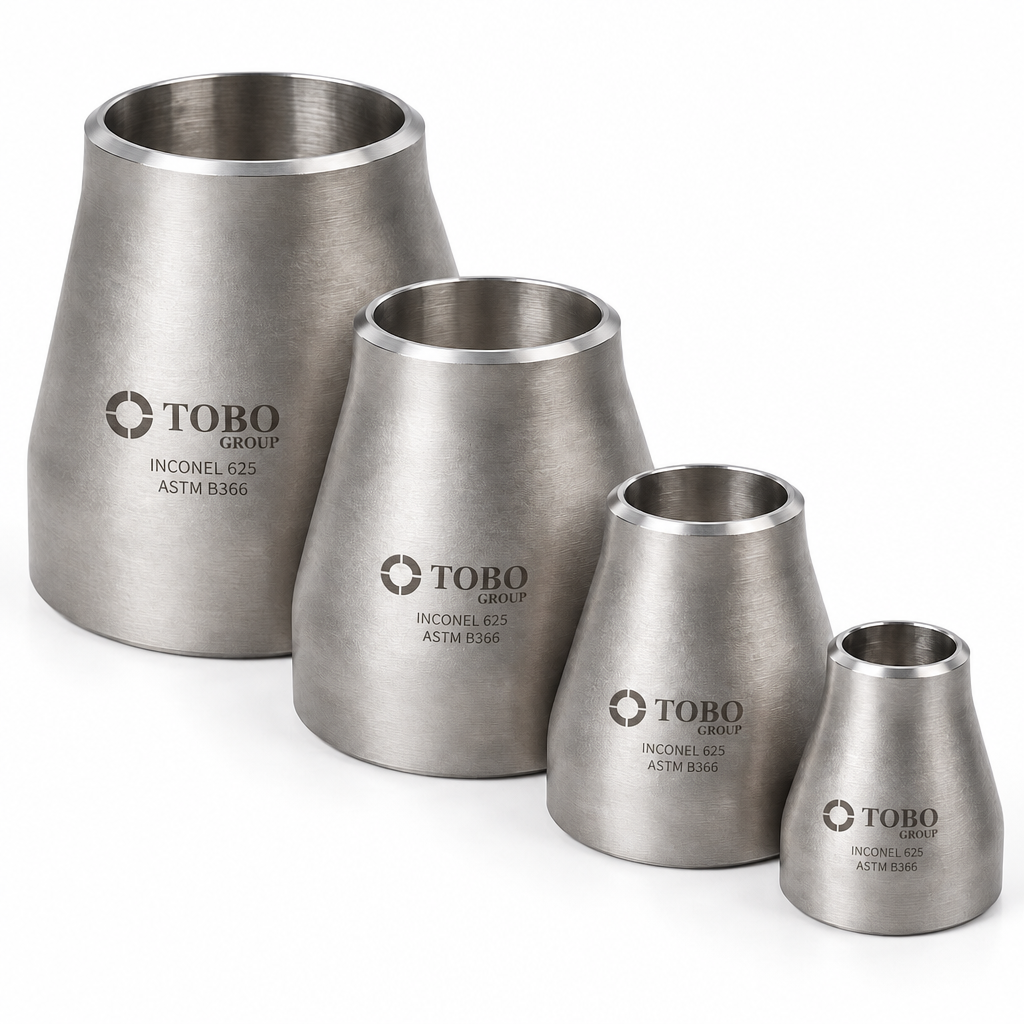
Core Industrial Advantages
1. Exceptional corrosion resistance across all media
Under extreme operating conditions—such as strong oxidizing/reducing acids (hydrochloric acid, sulfuric acid, hydrofluoric acid, phosphoric acid), high-concentration chlorides, wet chlorine gas, and hydrogen sulfide (H₂S)—it demonstrates exceptional resistance to general corrosion, completely resolving the common issues of pitting, crevice corrosion, and stress corrosion cracking (SCC) typically associated with conventional stainless steel.
2. Ultra-wide Temperature Range and Exceptional High-Temperature Strength
From cryogenic environments to ultra-high temperatures exceeding 1,000 degrees, it maintains extremely high yield strength, tensile strength, and excellent resistance to creep fracture and thermal fatigue, eliminating material embrittlement or plastic deformation caused by temperature changes.
3. Optimized Hydrodynamics and Resistance to Erosion and Wear
Precision forming processes ensure smooth transitions on the inner wall and strict concentricity/eccentricity tolerances, effectively suppressing fluid vortices and pressure drops during pipe diameter contraction and expansion. This significantly reduces the risk of erosion-corrosion caused by high-velocity media or particulate-laden fluids.
4. High-Pressure Safety and Zero Leakage Under Extreme Conditions
Utilizing precision seamless extrusion or full-penetration butt-welding processes, the material features a dense and uniform microstructure that strictly complies with ASME B16.9 and NACE MR0175 standards for acidic environments, ensuring structural integrity and sealing reliability under high pressure and alternating stresses.
5. Exceptionally Long Service Life and Lower Total Life-Cycle Costs
Compared to conventional alloys, nickel alloy pipe fittings offer a service life that is several times longer in high-risk, highly corrosive environments, significantly reducing unplanned downtime, the risk of media leaks, and the costs associated with frequent replacement and maintenance, thereby delivering an excellent overall return on investment (ROI) for plants.
1. Comprehensive Product Specification & Manufacturing Scope
|
Technical Parameter |
Engineering Standards & Detailed Capabilities |
|
Product Classification |
Industrial Butt-Weld Reducers (Concentric Reducer - CR / Eccentric Reducer - ER) |
|
Manufacturing Methods |
• Seamless (SMLS): Hot extrusion, cold mandrel drawing, hydraulic forming, CNC finish machining (1/2" – 12" NB / DN15 – DN300) |
|
Size & Dimensional Range |
• Nominal Pipe Size (NPS): 1/2" ×× 3/8" NB up to 24" × 20" NB (Standard step-down and multi-step custom reduction) |
|
Wall Thickness Schedules |
• Standard Schedules: SCH 5S, SCH 10S, SCH 20, SCH 40S/STD, SCH 80S/XS, SCH 120, SCH 160, SCH XXS |
|
Design & Dimension Standards |
• ASME / ANSI: ASME B16.9 (Factory-Made Wrought Butt-Welding Fittings), MSS SP-43 (Lightweight Corrosion Resistant Fittings), MSS SP-95 |
|
Material Specification |
ASTM B366 / ASME SB366 (Standard Specification for Factory-Made Wrought Nickel and Nickel Alloy Fittings) |
|
End Preparation & Beveling |
• Standard Butt Weld (BW): Beveled to ASME B16.25 — Bevel Angle: 37.5∘±2.5, Root Face: 1.6 mm±0.8 mm (1/16"±1/32"), Root Gap: 1.6 mm±0.8 mm |
|
Heat Treatment (Metallurgy) |
• Solution Annealing (Solid Solution): Rapid water quench from 1050∘C−1180∘C to dissolve carbide/intermetallic precipitate phases |
|
Surface Finish & Pickling |
• Pickling & Passivation: ASTM A380 / ASTM A967 acid pickled to eliminate free iron and weld discoloration |
2.Alloy Grades, Cross-Reference & Mechanical Properties
|
Trade Name / Series |
ASTM B366 Grade |
UNS Number |
Werkstoff Nr. (DIN/EN) |
Typical Yield Strength Rp0.2 (MPa) |
Tensile Strength Rm (MPa) |
Min. Elongation A5(%) |
Service Temp. Range (∘C) |
|
Hastelloy® C-276 |
WPHC276 / CRHC276 |
N10276 |
2.4819 (NiMo16Cr15W) |
≥355 |
≥790 |
≥40 |
−196 to +1040∘C |
|
Hastelloy® C-22 |
WPHC22 / CRHC22 |
N06022 |
2.4602 (NiCr21Mo14W) |
≥350 |
≥760 |
≥45 |
−196 to +1100∘C |
|
Hastelloy® B-2 / B-3 |
WPHB / WPHB-3 |
N10665 / N10675 |
2.4617 / 2.4600 |
≥350 |
≥760 |
≥40 |
−196 to +815∘C |
|
Inconel® 625 |
WPNCMC / CRNCMC |
N06625 |
2.4856 (NiCr22Mo9Nb) |
≥415 |
≥825 |
≥30 |
−196 to +980∘C |
|
Inconel® 600 |
WPNCI / CRNCI |
N06600 |
2.4816 (NiCr15Fe) |
≥240 |
≥550 |
≥30 |
−196 to +1150∘C |
|
Incoloy® 825 |
WPNICMC / CRNICMC |
N08825 |
2.4858 (NiCr21Mo) |
≥240 |
≥585 |
≥30 |
−196 to +540∘C |
|
Incoloy® 800 / 800H |
WPNIC / WPNICH |
N08800 / N08810 |
1.4876 / 1.4958 |
≥205 |
≥520 |
≥30 |
Cryogenic to +1000∘C |
|
Monel® 400 |
WPNM / CRNM |
N04400 |
2.4360 (NiCu30Fe) |
≥195 |
≥480 |
≥35 |
−196 to +480∘C |
|
Pure Nickel 200 / 201 |
WPN / WPNL |
N02200 / N02201 |
2.4066 / 2.4068 |
≥105 |
≥380 |
≥40 |
Sub-zero to +650∘C |
|
Alloy 20 (Carpenter 20) |
WP20CB |
N08020 |
2.4660 (NiCr20CuMo) |
≥240 |
≥550 |
≥30 |
Ambient to +500∘C |
3.Dimensional Tolerances (as per ASME B16.9 Standard)
|
Nominal Pipe Size (NPS) |
Outside Diameter at Bevel (DL/DS) |
Inside Diameter at End (dL/dS) |
Wall Thickness (t) |
Center-to-End Length (H) |
Angularity / Off-Square (Q) |
|
1/2" to 2-1/2" |
+1.6 mm/−0.8 mm |
±0.8 mm |
Min. 87.5% of nominal (t≥0.875×tnom) |
±1.6 mm |
≤0.8 mm |
|
3" to 3-1/2" |
±1.6 mm |
±1.6 mm |
Min. 87.5% of nominal (t≥0.875×tnom) |
±1.6 mm |
≤1.6 mm |
|
4" to 8" |
+2.4 mm/−1.6 mm |
±1.6 mm |
Min. 87.5% of nominal (t≥0.875×tnom) |
±1.6 mm |
≤1.6 mm |
|
10" to 18" |
+4.0 mm/−3.2 mm |
±3.2 mm |
Min. 87.5% of nominal (t≥0.875×tnom) |
±2.4 mm |
≤2.4 mm |
|
20" to 24" |
+6.4 mm/−4.8 mm |
±4.8 mm |
Min. 87.5% of nominal (t≥0.875×tnom) |
±2.4 mm |
≤3.2 mm |
4. Chemical Resistance & Media Suitability Matrix
|
Corrosion Environment & Medium |
Recommended Nickel Alloy Grade |
Failure Mechanism Prevented |
|
Hydrochloric Acid (HClHCl) & Wet Chlorine Gas |
Hastelloy® B-3, Hastelloy® C-276 |
Eliminates rapid uniform attack & active hydrogen embrittlement |
|
Sulfuric Acid (H2SO4H2SO4) & Phosphoric Acid (H3PO4H3PO4) |
Incoloy® 825, Alloy 20, Hastelloy® C-22 |
Prevents intergranular corrosion and boiling-acid thinning |
|
Hydrofluoric Acid (HFHF) & Marine Seawater |
Monel® 400, Monel® K-500 |
Exceptional resistance to severe cavitation and pitting in high-velocity brine |
|
Sour Oil & Gas (H2S/CO2H2S/CO2 / Chlorides) |
Inconel® 625, Hastelloy® C-276 |
Fully compliant with NACE MR0175; zero Sulfide Stress Cracking (SSC) |
|
Caustic Alkalis (NaOH,KOHNaOH,KOH across all conc.) |
Pure Nickel 200 / Nickel 201 |
Total immunity to caustic embrittlement / alkaline stress cracking |
|
High-Temperature Oxidation & Carburization |
Inconel® 600, Incoloy® 800H / 800HT |
Forms adherent refractory oxide scale preventing catastrophic spallation |
5. Quality Assurance, Testing Matrix & Documentation
|
Inspection & Quality Control Category |
Testing Standard / Method |
Acceptance Criteria & Scope |
|
100% Positive Material Identification (PMI) |
ASTM E1476 / Portable XRF & OES Analyzers |
Zero grade mix-up; 100% verification of chemical elements (Ni, Cr, Mo, Fe, Cu, W) |
|
Radiographic Testing (RT / X-Ray) |
ASME Section V, Article 2 / ASME Section VIII Div. 1 UW-51 |
100% RT examination on all longitudinal and circumferential welded joints |
|
Liquid Penetrant Examination (PT) |
ASTM E165 / ASME Section V, Article 6 |
100% PT on bevel ends, radius transitions, and root weld surfaces (Zero linear defects) |
|
Ultrasonic Testing (UT) |
ASTM A388 / ASME Section V, Article 4 |
Full volumetric examination for internal laminations, inclusions, and wall thickness uniformity |
|
Intergranular Corrosion Test (IGC) |
ASTM G28 (Methods A & B) / ASTM A262 |
Verification of post-weld solution annealing; zero sensitized grain boundaries |
|
Critical Pitting & Crevice Corrosion Test |
ASTM G48 (Methods A, B, C, D) |
Ferric chloride immersion testing verifying PREN performance |
|
Mechanical & Destructive Tests |
ASTM A370 / ASTM E8 / ASTM E23 |
Tensile, yield, elongation, reduction of area, Charpy V-Notch impact (down to −196∘C−196∘C) |
|
Hydrostatic Proof / Burst Test Verification |
ASME B16.9 Clause 2.2 / ASME B31.3 |
Calculation validation ensuring fitting withstands 1.5×× design pressure without leakage |
|
Certifications & Traceability Dossier |
EN 10204 Type 3.1 / 3.2 |
Full Mill Test Certificate (MTR) showing Heat No., raw material origin, chemical composition, mechanical tests, heat treatment chart, and third-party inspection endorsement (TÜV, DNV, SGS, BV, Lloyd's) |
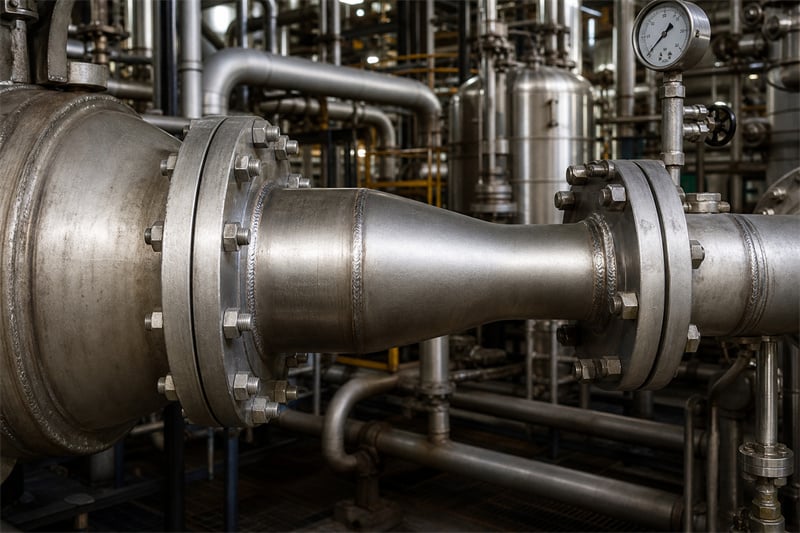
Chemical and Petrochemical Process Industries
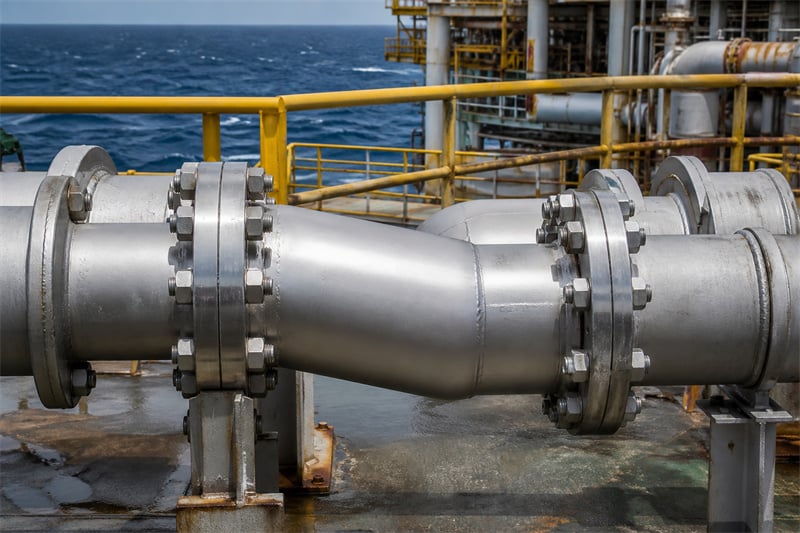
Offshore Engineering and Seawater Systems
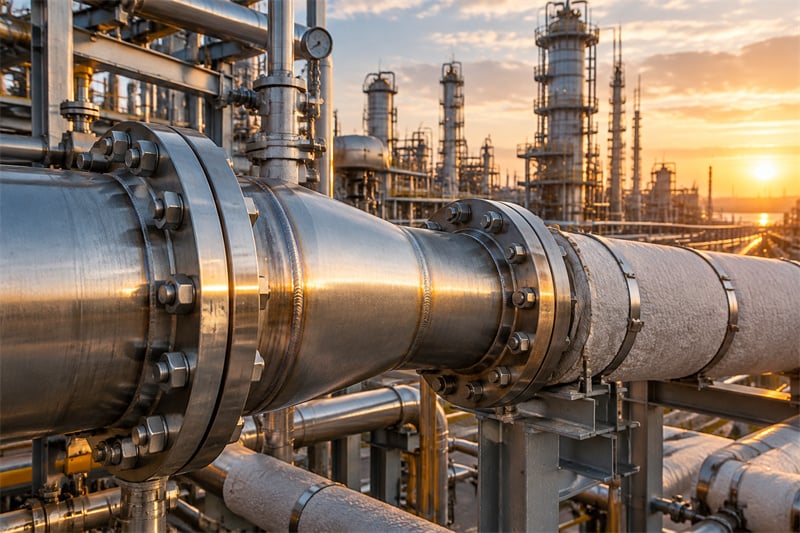
Oil and Gas and Refining and Petrochemical Industries
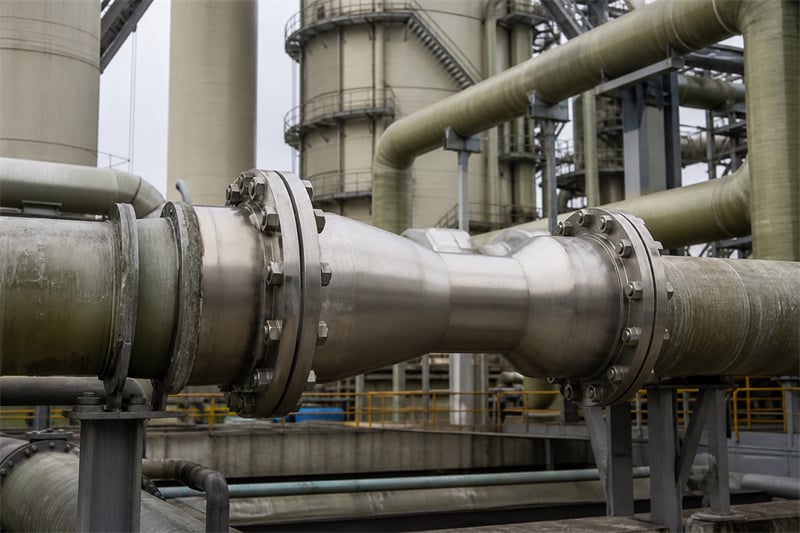
Environmental Protection and Flue Gas Treatment (FGD/Exhaust Gas Purification)
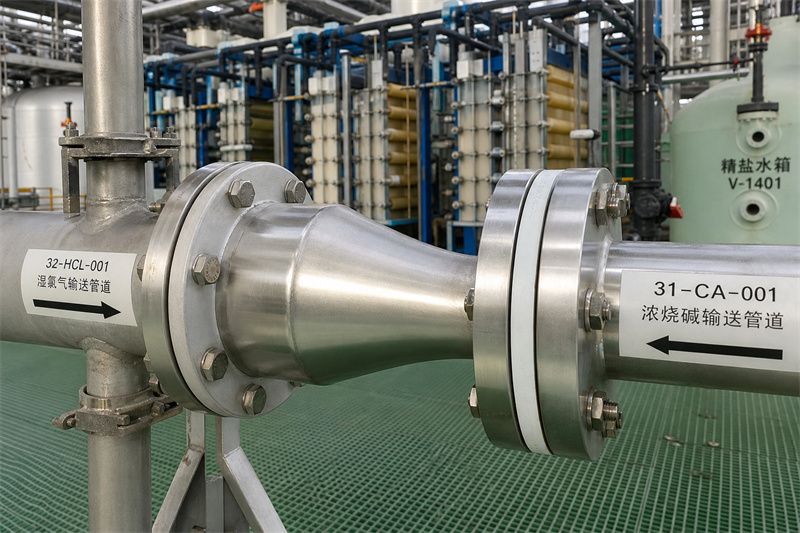
Chlor-Alkali and Soda Ash Production Industries
Pharmaceutical Industry
Pulp and Paper
Nuclear Power and Nuclear Fuel Reprocessing
Electricity and Desalination
Nickel alloy reducers are suitable for marine, chemical, and chlorine-containing environments where 304/316L austenitic stainless steel is prone to failure. Typical grades, such as Monel 400, Inconel 625, and Hastelloy C-276, offer higher inherent corrosion resistance in seawater, mixed acids, and high-temperature corrosive environments, thereby reducing the need for preventive replacements based on corrosion allowances.
Reducers are pipe joints subjected to sudden changes in flow velocity, pressure fluctuations, and thermal cycling. Integral forging ensures continuous metal flow lines, refined grain structure, and uniform wall thickness, reducing the risk of shrinkage porosity and heat-affected zones from welding. This makes them suitable for high-pressure, high-temperature, and pipelines with frequent pressure fluctuations.
Products are manufactured in accordance with the ASTM B366 forged butt-weld pipe fitting system, with dimensions conforming to ASME B16.9, covering specifications such as NPS 1/2–24 and SCH 5S–XXS. Products can be supplied with EN 10204 Type 3.1 material certificates, PMI, and non-destructive testing (NDT), and meet the requirements of NACE MR0175/ISO 15156 for acidic service and ASTM G28/A262 for intergranular corrosion testing.
The core selling point should not be limited to “corrosion resistance,” but rather expressed as: reducing replacement cycles and the risk of unplanned downtime caused by chloride-induced stress corrosion cracking in seawater, acidic, and high-temperature environments, thereby increasing the likelihood of being specified in project specifications and included in EPC procurement lists.

Copyright © TOBO GROUP All Rights Reserved - Privacy Policy

 EN
 AR
 BG
 HR
 CS
 DA
 NL
 FI
 FR
 DE
 EL
 HI
 IT
 JA
 KO
 NO
 PL
 PT
 RO
 RU
 ES
 SV
 TL
 VI
 TH
 TR
 GA
 CY
 BE
 IS